MR ALADDIN : 18816899059@163.com
MR AU: auvuchi@163.com

0086-18816899059
0086-15018408881


OG-RM9070 Three-station high speed thermoforming machine

一、 技术参数 Technical parameter
适应的材料 Suitable materials | PP、 HIPS、 PET、 PS |
适应片材宽度 Sheet width | 500mm-840mm |
最大成型面积 Max.Forming area | 900mm×700mm |
最小成型面积 Min.Forming area | 700mm×500mm |
制品成型高度 Height of forming | ≤100mm |
最高生产速度 Max. Rate of production speed | ≤40Times/min |
开合模高度 Moving Mould Distance | 上动模台行程≤150mm,下动模台行程≤ 150mm The stroke of the upper and lower moving mold table≤150mm |
最大锁模力 Max.clamping force | 65T |
电源功率 Electric power | 183KW (heating power) + 50KW (motor power) =233KW Normal operating power 55KW/H |
电源规格 Power supply specification | AC380v50Hz,4P(50mm2)+1PE(25mm2)three-p hase five-wire system |
气源压力 Air pressure | 0.7MPa |
机器尺寸 Machine size | 11.0M(长 L)*2.80M(宽 W)*3.20M(高 H) |
整机重量 Total weight | About 19ton |
主要电气元件清单
Main Electrical components list
NO | Name | Manufacturer | Origin | ||||
1 |
触摸屏 Touch screen |
|
China | ||||
2 | PLC 可编程序控制器 PLC programmable logic controller |
|
Japan | ||||
3 | 定位模块 Positioning Module | ||||||
4 | 扩展通讯线 Extended communication lines | ||||||
5 | 扩展底板 Expansion backplane | ||||||
6 | 数字量输入模块Digital input module | ||||||
7 | 数字量输出模块 Digital output module | ||||||
8 | 主基板 Main board | ||||||
9 | PLC 电源 PLC power supply |
|
Taiwan, China | ||||
10 | 伺服电机 Servo motor |
|
Japan | ||||
11 | 伺服驱动器 Servo drives | ||||||
12 | 温度控制模块 Temperature control module |
|
China | ||||
13 |
减速机 Reducer |
|
America | ||||
14 | 总开关 Main breaker |
. |
France | ||||
15 | 空气开关 Air switch | ||||||
16 | 可调断路器 Adjustment breaker | ||||||
17 | 接触器 Contactor | ||||||
18 | 常开点 Open point | ||||||
19 | 通用继电器 Purpose relay | ||||||
20 | 电气维修灯管 Lamp | ||||||
21 | 带灯按钮 Buttons | ||||||
22 | 急停开关 Stop switch | ||||||
23 | 主令开关 Main switch | ||||||
24 | 报警灯 Warning lights | ||||||
25 |
真空泵Vacuum pump |
|
China | ||||
26 | 收卷电机 Rewinding motor |
|
China | ||||
27 | 放卷电机 Unwinding motor | ||||||
28 | 链轨调节电机 Chain adjustment motor | ||||||
29 | 模台调节电机 Mold table adjustment motor | ||||||
30 | 温控模块 Temperature controller |
|
Taiwan,China | ||||
31 | 限位开关 Limit switches | ||||||
32 | 感应开关 Sensor Switch | ||||||
33 | 固态继电器 Solid State Relays | ||||||
34 |
加热瓦 Heater |
|
Ireland/China | ||||
35 |
成型阀 Forming valve |
|
America | ||||
36 |
气动原件 Pneumatic components |
|
Taiwan, China | ||||




整机细节描述
Detailed description of the whole machine
1. 放片装置
Sheet setting device
1. 1由气缸提升上料;
Lift feeding by cylinder
1.2 适用片材直径 1 米以内;
Sheet max. Diameter:≤1000mm
1.3 由光电传感器来确定预送料的长度;
The length of pre-feed is determined by photoelectric sensor;
1.4 送片由电机驱动一对夹送辊, 具有自动加减速功能, 带送片自动控制。
The feeding is driven by a motor with a pair of clamping rollers, with automatic acceleration and deceleration function, with automatic control of the feeding sheet.
2. 送片装置 Feeding device
2.1 送片装置采用日本安川伺服电机配 GNORD 硬齿面斜锥齿减速机驱动;
The feeding device adopts YASKAWA servo motor and GNORD hard tooth surface inclined bevel tooth reducer drive.
2.2 链轨材料为阳极硬化处理的一体成型铝型材,带通水冷却装置, 并配上水压压力表;
The chain rail is an integrated forming aluminum profile with anode hardening treatment, with water cooling device, and equipped with water pressure gauge.
2.3 配有 3 段式为自动调整功能, 由于 3 台电机在前中后 3 点单独调节, 也可以同步调节。可选配片材下垂后的退炉停机保护装置。
Equipped with a 3-stage automatic adjustment function, because the three motors are individually adjusted in the front, middle and back points, it can also be adjustment synchronously. Optional furnace shutdown protection device after sheet sagging.


3. 加热系统
Heating system
3.1 加热区探头瓦片采用爱尔兰 CERAMICX 进口陶瓷加热片, 其余采用江苏天宝陶瓷加热片
The heating zone probe tiles adopts ceramic heating plate imported from Ireland CERAMICX, and the rest adopts Jiangsu Tianbao ceramic heating plate;
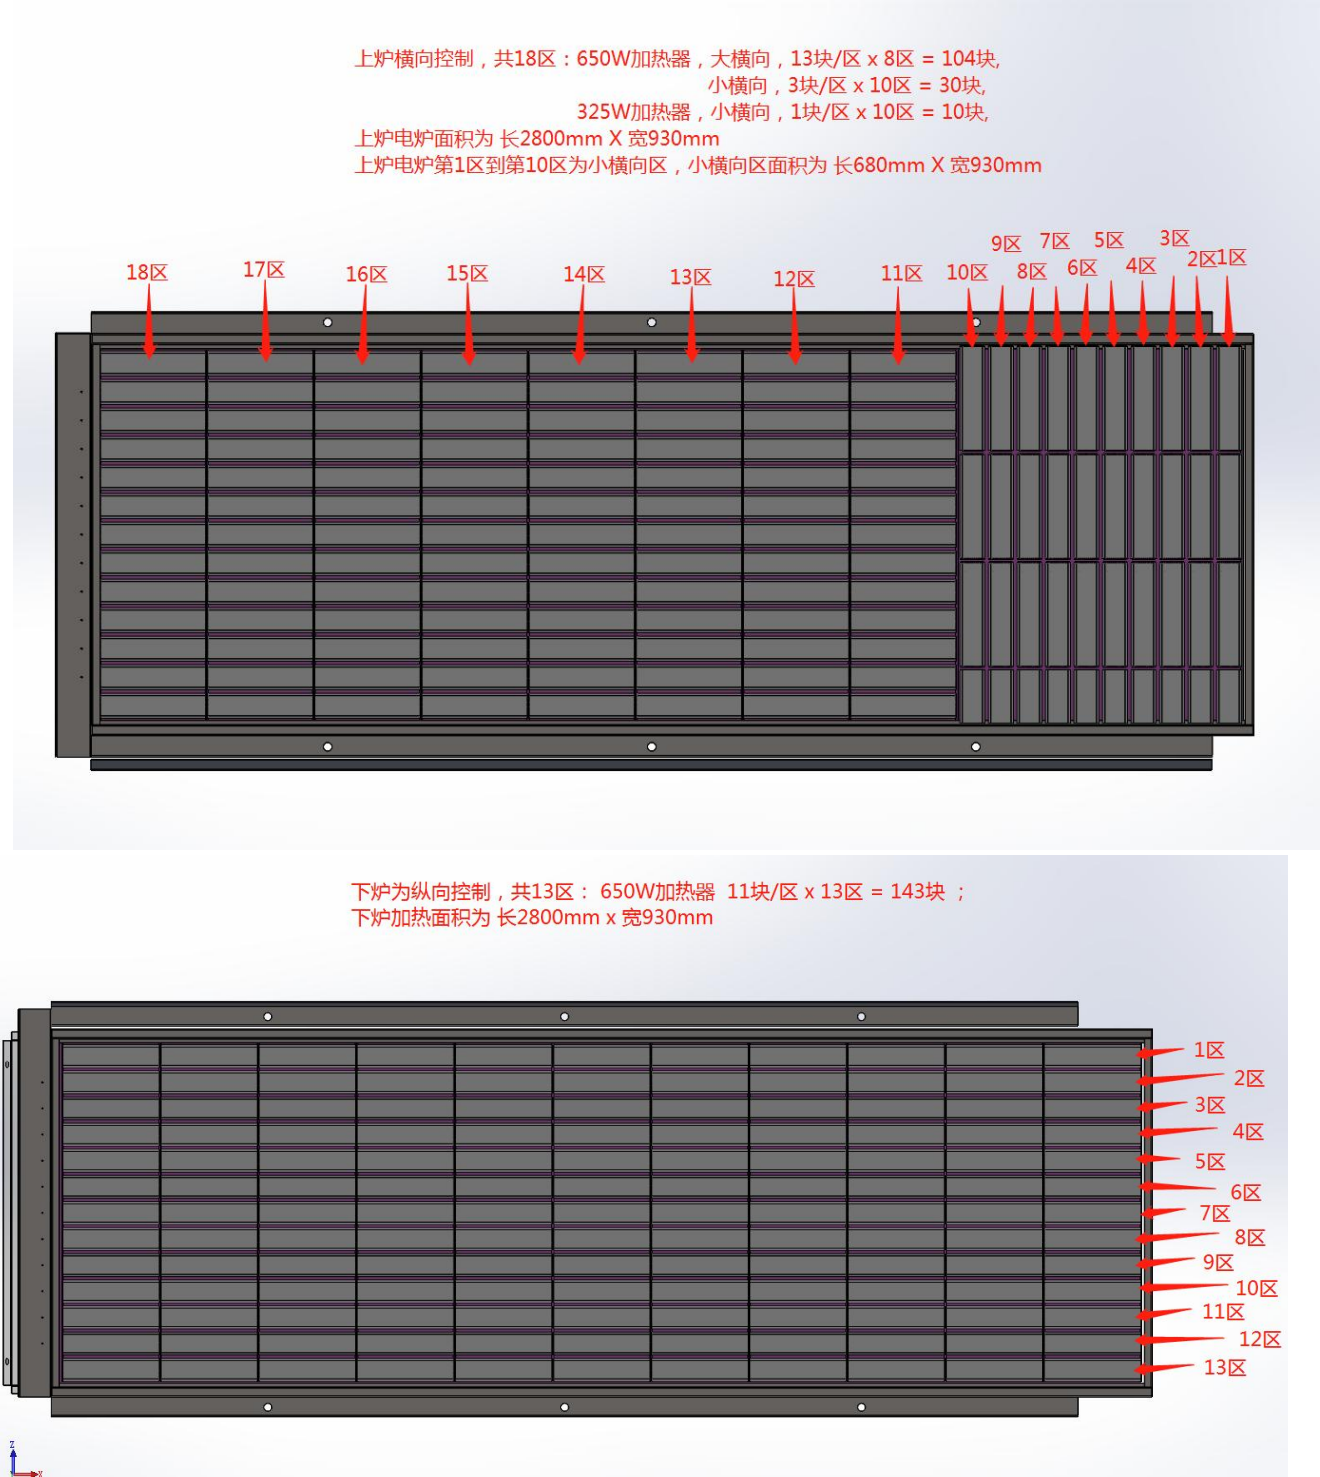
3.2 电热规格采用: 上炉 104 块 650W 横向布置, 30 块 650W, 10 块 325W 横向布置, 下炉143 块 650W 纵向布置。 共 277 块 650W, 10 块 325W, 总功率 183KW;
The electric heating specifications adopt: 104 pieces of 650W horizontal arrangement of the upper furnace, 30 pieces of 650W, 10 pieces of 325W in horizontal arrangement, and
143 pieces of 650W longitudinal arrangement of the lower furnace. A total of 277 blocks of 650W, 10 pieces of 325W, a total power of 183KW;
3.3 温度控制系统由温控器控制 SSR 固态继电器, 可以精准的控制温度, 参数设定在触摸屏上设定, 并带有断线报警及电流检测功能, 可自动判断某区的加热器的正常工作;
The temperature control system is controlled by the thermostat SSR solid state relay, which can accurately control the temperature. The parameter are setting on the touch screen, with a wire break alarm, which can automatically judge the normal operation of the heater in a certain area.
3.4 框架采用铝型材拼焊结构;
The frame adopts aluminum profile splicing structure;

(温控控制系统细节图 Detail diagram of the temperature control system)

(电炉加热瓦细节图 Detail of electric furnace heating tiles)

(铝合金电炉架 Aluminum alloy electric furnace frame)
4. 成型工位, 裁切工位:
Forming station, cutting station:
4.1 机架采用国标 125# H 型钢与 120#槽钢、 钢板组合焊接定型处理而成;
The frame is made of national standard 125# H steel, 120# channel steel and steel plate combination welding and shaping treatment.
4.2 工位站开合模结构由下固定底座、下开合模连杆支撑组件, 下开合模动模台、上固定座、上开合模连杆支撑组件、 上开合模动模台、 及安装模具模架及 4 条立柱组成;
The opening and closing mold structure of the station is composed of the lower fixed base, the lower opening and closing mold connecting rod supporting assembly, the lower opening and closing mold moving mold platform, the upper fixing seat, the upper opening and closing die connecting rod support assembly, the upper opening and closing die moving die platform, and install the mold base mold mold frame and 4 columns.
4.3 焊接式底座、 动模台、 上模台及模架的安装基准面由大型进口数控加工中心一体加工后组装而成, 从而提高设备组装精度, 同时也提高设备生产过程的稳定性;
The installation datum of welding base, moving mold table, upper mold table and die frame is assembled by a large imported CNC machining center after integrated processing, so as to improve the accuracy of equipment assembly and the stability of the equipment production process.
4.4 立柱采用优质钢经调质后表面镀硬铬精磨而成;
The column is made of high quality steel after hard chrome plating and fine grinding on the surface after quenching and tempering.
4.5 动模台由伺服电机驱动曲臂连杆结构进而推动五支点进行开合模,上下开合模动力采用日本安川 11千瓦, 伺服电机总线通讯控制配 GNORD 硬齿面斜锥齿减速机驱动, 所有连杆采用铜套传动, 传动效率高, 减少机械磨损, 便于维护; 动模台开合行程≤150mm;
The moving mold platform is driven by the servo motor toggle connecting rod structure and then drives the five fulcrum to open and close the mold, the upper and lower opening and closing mold power adopts the YASKAWA 11 kW, the servo motor bus communication controller is driven by the GNORD hard tooth surface inclined cone tooth reducer, all connecting rods are driven by copper sleeve, which has high transmission efficiency, reduces mechanical wear and is easy to maintain. Opening and closing stroke of moving mold table ≤150mm;
4.6 上模台数控电动调模, 调模精度±0.03mm;
CNC electric mold adjustment on the mold platform, the mold adjustment accuracy is ± 0.03mm


(五支点结构细节图: 开模/合模状态
Detail diagrams of five-piovt strcture: Open/Close mold state)

5. 制品堆叠工位 Product stacking station
制品在成型模内留点裁切,开模后由送片链条输送到堆叠工位后, 由伺服电机配利茗行星减速机驱动同步带完成升降的动作向下顶断并垒叠,在垒叠过程中,有真空吸盘装置将制品平稳叠放在输送带上; 输送带由伺服电机驱动, 平稳的将制品输送出。
The product is cut in the molding die, and after the mold is opened, it is transported to the stacking station by the feeding chain. The servo motor with the Liming planetary reducer drives the synchronous belt to complete the lifting action, break it downward and stack it. During the stacking process, a vacuum suction cup device stacks the product steadily on the conveyor belt. The conveyor belt is driven by servo motors and convey the products smoothly .
6. 废边收卷装置 Waste material winding device
6.1 独立收卷装置一套; 收卷装置由恒张力模式收卷;
One set of independent winding device. The winding device is winding by constant tension mode;
7.润滑系统
Lubrication system
7.1 模台润滑系统采用全自动润滑装置, 注油频率在人机界面上设定。
The mold lubrication system adopts a fully automatic lubrication device, and the oil injection frequency is set on the touch screen.

8. 气动元件
Pneumatic element
8.1 气动元件中成型阀与真空阀采用美国 MAC 大流量电控阀,其余气动元件均采用台湾亚德客品牌;
The forming valve and vacuum valve in the pneumatic components adopt the American MAC high-flow electric control valve, and the rest of the pneumatic components adopt the Taiwan AirTAC brand;
9. 控制系统
Control system
9.1 整机控制系统人机界面为可推拉的滑轨式安装, 以方便操作;
The touch screen of the whole machine control system is a sliding rail installation that can be pushed and pulled to facilitate operation.
9.2 控制系统采用日本基恩士运动控制器, 对各个伺服电机进行全闭环的控制;
The control system adopts the Japanese KEYENCE motion controller to control each servo motor in a full closed loop;
9.3 配备 15 寸昆仑通态人机界面; Equipped with 15-inch Kunlun Tongtai MCGS touch screen.
9.4 开关、 按钮、 断路器、 接触器及中间继电器均采用法国施耐德品牌;
Switches, buttons, circuit breakers, contactors and intermediate relays are all made of French Schneider brand.
9.5 接近开关及传感器采用台湾阳明品牌;
The proximity switch and sensor adopt Taiwan FOTEK.
9.6 温控系统采用汇川温控器, 继电器采用台湾阳明 SSR 固态继电器;
The temperature control system adopts INOVANCE thermostat, and the relay adopts Taiwan FOTEK SSR solid state relay;
9.7 控制柜置于设备的内部, 具有更方便的维护型, 控制柜配备了空调恒温恒湿系统。
The control cabinet is placed inside the equipment and has a more convenient maintenance type. The control cabinet is equipped with an air conditioning constant temperature and humidity system


10.电炉排列图及功率分布 Electric furnace arrangement diagram and power distribution
FOB China.
- Delivery time: The Seller will hand over the goods to the buyer after 90 business days, excluding Saturdays, Sundays and public holidays (1-5 days for ship departure and customs clearance) Both parties sign the contract and the seller receives the full payment
- Place of delivery: at the buyer's address, the buyer will receive the goods and put in place to install
Set up :
- The Seller completes the installation of the equipment for the buyer within one week from the date the equipment is returned to the buyer's location.
Acceptance :
l Equipment that is considered valid must meet the following requirements:
l ü Specifications and functions of the machine match the content of this contract.
l ü Electrical, mechanical and control systems run smoothly.
l ü Run out sample products as required.
l ü Must have a certificate of quality of the place of production and documents attached to the machine.
ARTICLE 2: PAYMENT METHOD
v The buyer makes payment to the seller in 02 times by transfer to the seller's account.
v v First time: The buyer advances to the seller 30% of the contract value, right after the two parties sign the contract.
v v 2nd time: The buyer pays the seller 70% of the contract value, immediately after the seller sends the video of the acceptance of the camera and the picture, sends the standard sample to the buyer (IF YES). The seller will send a notice of delivery to the buyer.
ARTICLE 3: WARRANTY
Warranty period: within 12 months from the acceptance date of the equipment.
During the warranty period, if the equipment is defective by the manufacturer of the Seller, the Seller is responsible for the presence at the purchaser factory within 48 hours of being notified to repair the equipment. All costs incurred will be borne by the Seller.
(If the device is faulty by the user or is affected by unintended issues such as
Unstable electrical lines, collisions, natural disasters, unclean hygiene, the purchaser must be fully responsible for paying for repair and other replacement expenses)
ARTICLE 4: BUYER'S LIABILITY
6.1 Provide auxiliary systems and handover surface installation equipment. The auxiliary systems include: supply of supplies and preparation of 3 Phase 220V / 50Hz power supply systems for electrical appliances including switches, sockets, power wires, Electric three-phase electric switches, electric lines, steam-lines, gas lines, gas valves, pipes, elbows,
The buyer is responsible for dropping the item at the buyer's address to the correct location
6.2 The purchaser shall be responsible for sending the representative to receive the goods and taking over the test when the equipment has been installed and the instruction manual is used.
6.3 The buyer pays the seller under Article 4 of this contract.
6.4 The expenses such as as airplane, visa, travel expenses,other expenses for foreign engineers in china will be paid by the Seller.
6.5 The Other expenses such as pick up and see off ,dining, hotel for technical will be charged by the buyer,the buyer will be pay for the engineer 200USD each day .
ARTICLE 5: SELLER'S LIABILITY
7.1 Commitment to deliver the equipment to the purchaser in accordance with the type and design of this contract.
7.2 Vendors undertake:
Asian. Ensure time and progress of equipment handover
B. Assurance of quality and content in accordance with agreement requirements.
C. Vendors nominate technical staff to assist, install and guide the buyer to operate and use the equipment well when installing the machine.


点击右上角
分享给朋友吧
© 2025 GUANGDONG CHAMPION AUTOMATION TECHNOLOGY CO.,LTD all rights reserved
Contact us
GUANGDONG CHAMPION AUTOMATION TECHNOLOGY CO.,LTD
Telephone: 020-38912384
Email :
Sales@champion-automation.com
Fax: 020-38912463
Tel: 0086-18816899059, 15018408881
Add:Room 2116,No 101-1 ,Li Xin 12th street, Xin Tang Town, Zeng Cheng District, Guang Zhou, Guang Dong province, China